Alright, let’s cut to the chase—if you’re here because you’ve got new cold rolling equipment coming in and you’re stressing over how to get it up and running without messing things up, you’re in the right spot. I’ve been selling cold rolling gear for over a decade, and let’s be real: installation is where a lot of folks either save big or drop a ton of cash on avoidable mistakes. No fancy jargon, just the real steps we walk our clients through every single time, plus the pro tips only veteran suppliers know. Cold Rolling Equipment
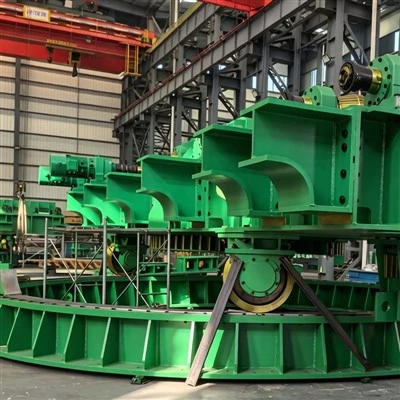
First off, let’s get one thing straight: cold rolling isn’t your run-of-the-mill machine—this stuff handles metal at room temp, so every inch has to be aligned, tensioned, and calibrated perfectly. Skip a step here, and you’re looking off-spec coils, broken rollers, or even safety hazards down the line. I’ve seen a client try to rush the anchor bolt tightening and end up with a $12k roller replacement after a week of runs. Don’t do that.
Let’s start with the pre-install prep, because this is where 50% of the work happens before the gear even touches your floor. A lot of clients sleep on this and then panic when the crane’s waiting and the foundation’s not ready. First up: the foundation check. You can’t set a $500k rolling mill on a concrete slab that’s got a 0.5mm dip in the middle. Here’s the tea: we always send our in-house techs out 7–10 days before delivery to measure the foundation. They use a laser level (no old-school string lines here) to check flatness, compression strength, and anchor bolt holes. Wait—anchor bolts! They need to be threaded clean, no debris, and spaced exactly to the equipment’s drawings. I once had a client with holes that were 2mm off, and we had to custom-make spacers at 2 a.m. to get the mill on the pad. Not fun, and it set their install back 3 days. Also, clear the path from the loading dock to your production floor—those heavy components (like the work roll stand) are 10+ tons, so no random pallets or leftover scrap blocking the way. And don’t forget utilities: you need clean, dry compressed air (no moisture, that’ll mess up the hydraulic system), a stable 480V power supply (we always require a dedicated circuit for the mill), and a water line for cooling the rollers. Skimp on the air dryer, and you’ll be replacing solenoids in 6 months.
Next step: offloading and positioning. When the crane shows up, don’t let the yard guys wing this—our techs are there to signal every move because these parts are delicate. For example, the main roll stand is super heavy, but it’s also got precision-machined surfaces on the bottom that can get dinged if the spreader bars aren’t positioned right. We use nylon slings, not steel, to avoid scratching the frames. Once it’s on the foundation, it’s not just setting it down—you need to get it roughly lined up with the alignment reference points (the we put those in the foundation before pour, fyi). This is where the heavy-duty jacks come in, not the small ones from your toolbox. Pro tip: mark the centerline of your production line on the floor before delivery—saves hours of moving the stand back and forth.
Now, the part everyone calls “make-or-break”: precision alignment. This is where the cold rolling magic starts, or fails. There are two main types here: horizontal alignment (making sure the roll stand is level left-to-right) and axial alignment (making sure it’s square with the direction the metal will feed). We use a laser alignment system—way more accurate than a dial gauge, and way faster. Wait, why does this matter? If your rolls are even 0.1mm off, the metal will bend to one side, you’ll get wavy edges, and you’ll have to scrap half the first batch. I remember a client that skipped laser alignment and ran 20 tons of scrap coil before they called us to fix it—cost them way more than hiring our techs to do it right the first time. Also, during alignment, we tighten the anchor bolts in a crisscross pattern, not all in a row—prevents the slab from shifting unevenly. Once the stand’s locked down, we attach the auxiliary parts: the uncoiler, recoiler, and the tension rolls. These have to be aligned to the main stand within 0.05mm, so we use the same laser reference all the way down the line. No cutting corners here—this is what keeps your coils straight and consistent.
After alignment, it’s time to hook up the systems and test the basics. First, the hydraulic system—this controls the roll gap and tension. We flush the lines first, because even a tiny piece of metal shavings can clog a solenoid and cause the mill to jam. Then we pressure test it, make sure there are no leaks. Next, the cooling system for the rolls—you have to run water through it for 30 minutes before powering on, to make sure there’s no blockage that’ll overheat the rollers (overheated rollers warp, and that’s a $20k fix). Then electrical: we connect the motor drives, plc, and sensors, and do a “soft start” to make sure everything’s communicating. Pro move here: we run a pressure test on the air system too—leaky lines will cause the pneumatic controls to act weird, leading to inconsistent tension.
Now, the fun part: commissioning with a test run. This is where we don’t just push a button and cross our fingers. First, we do a dry run with no metal—we cycle the uncoiler, recoiler, and roll gap controls 10 times to make sure everything moves smoothly. Then, we use a scrap coil (a cheap offcut, not production material) for a test pass. We start at half speed, monitor the thickness gauge, tension readings, and roll temperature. If there’s a wobble in the coil, we tweak the alignment a tiny bit. If the thickness is off, we adjust the roll gap via the PLC. I always tell clients: if the test run goes wrong, stop immediately—don’t keep running it, that’ll just make the fix harder. Once we get a perfect 10-meter strip, we crank it up to full speed. And before we leave, we train your operators for 4 hours—no “here’s a manual, figure it out.” We show them how to adjust tension, check for common issues, and do basic maintenance.
Wait, hold on—what about safety? I can’t skip this, because cold rolling equipment is no joke. All our installers follow OSHA rules, and we make sure all safety guards are on, emergency stops work, and operators know how to use PPE. One client forgot to lock the emergency stop during a test and almost got hurt—we’ve never left a site until everyone’s clear on safety protocols.
Now, why does all this matter to you? Because as your equipment supplier, we don’t just drop off a box and dip—we’re in it for the long haul. Rushing install, cutting corners on prep, or skipping alignment means you’re losing money on scrap, downtime, and repairs before you even start production. I’ve had clients that did their own install and had to call us back 2 weeks later to fix misalignment—they spent twice as much as if we’d done it right the first time.
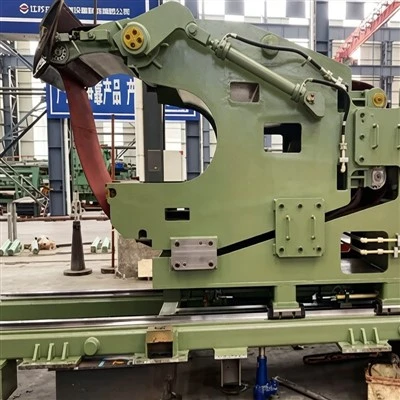
If you’re gearing up to get new cold rolling gear, or your current mill is giving you headaches and you need an upgrade, don’t wing this. Give us a holler to chat through your setup, answer any questions, and get a timeline that works for you. We bring all the tools, the techs, and the experience to get you up and running without the stress.
Heating Furnace References
- Cold Rolling Technology: Principles and Applications, Metalworking Industries Association, 2021
- Machinery Installation and Alignment Handbook, 3rd Edition, CRC Press, 2019
- OSHA Safety Standards for Metalworking Machinery, U.S. Department of Labor, 2022
Jiangsu Dongfang Whole-Set Equipment Manufacturing Group Co., Ltd.
We are one of the most professional cold rolling equipment manufacturers and suppliers in China, also support customized service. With abundant experience, we warmly welcome you to buy durable cold rolling equipment from our factory. If you have any enquiry about pricelist, please feel free to email us.
Address: No. 9, Industrial Park, Xinqiao Town, Jingjiang City, Jiangsu Province
E-mail: dfctwm@163.com
WebSite: https://www.dongfangequip.com/
